Corrugated Packaging for Food & Drink Manufacturers
Shelf-ready and transit packaging for high-throughput production lines. RightBox supplies and manages corrugated packaging for organisations where packaging is operationally critical.
Trusted by

What makes food and drink manufacturing packaging demanding.
- Packing-line speed and reliability
- Retailer shelf-ready requirements
- Promotional and seasonal volume swings
How RightBox helps.
- Specifications engineered for line performance
- Retail-ready formats aligned to retailer standards
- Forecast-led supply through peaks
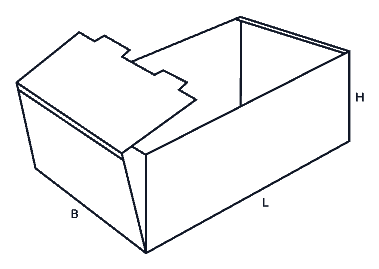
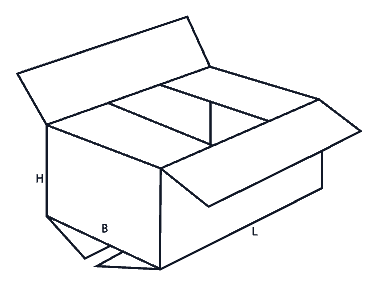
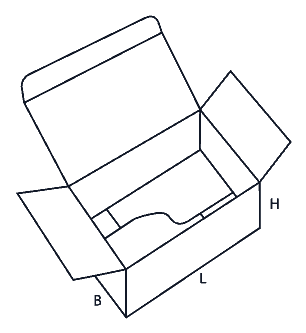
Box styles we commonly supply.
Every specification is confirmed against your product and supply chain. These are common starting points for the sector.
What to plan for.
01
Chilled and frozen storage reduces board compression strength
02
Packing-line performance depends on consistent board and dimensions
03
Shelf-ready packs must meet each retailer's requirements
04
Direct food contact needs food-safe liners or inner packs
Frequently asked questions
What corrugated packaging do food and drink manufacturing businesses use?
Common formats include FEFCO 0422 (shelf-ready trays built for retailer standards); FEFCO 0201 (outer transit cases for production and distribution); FEFCO 0713 (crash-lock cases for fast manual packing). The right choice depends on the product, packing process and distribution route.
Does RightBox manufacture the packaging?
No. RightBox manages supply through a network of 43 verified partner manufacturing sites in 7 countries, selecting the right partner for each specification.
Can you supply multiple sites?
Yes. RightBox works with organisations that operate multiple sites and countries, with harmonised specifications and one point of accountability.
Explore more sectors.
Let’s talk about your packaging.
Tell us about your sites, volumes and current suppliers. A specialist will review your requirements and arrange an initial conversation.